Assessing a supplier’s capacity for scaling CCD laser marking machine orders is hard quality management system 1. One unit built well says nothing about fifty, as buyers who visit our Dongguan factory often admit.
To assess a supplier’s capacity for scaling CCD laser marking machine orders, verify recent production records, confirm they can add lines and staff, check stock of lasers and CCD cameras, review past large-order delivery data, and lock delivery dates and quality standards into the contract.
Below, I walk through each of these checks in order. I also share the questions I would ask if I were sitting on your side of the table.
How can I verify a supplier's actual production capacity before placing a large CCD laser marking machine order?
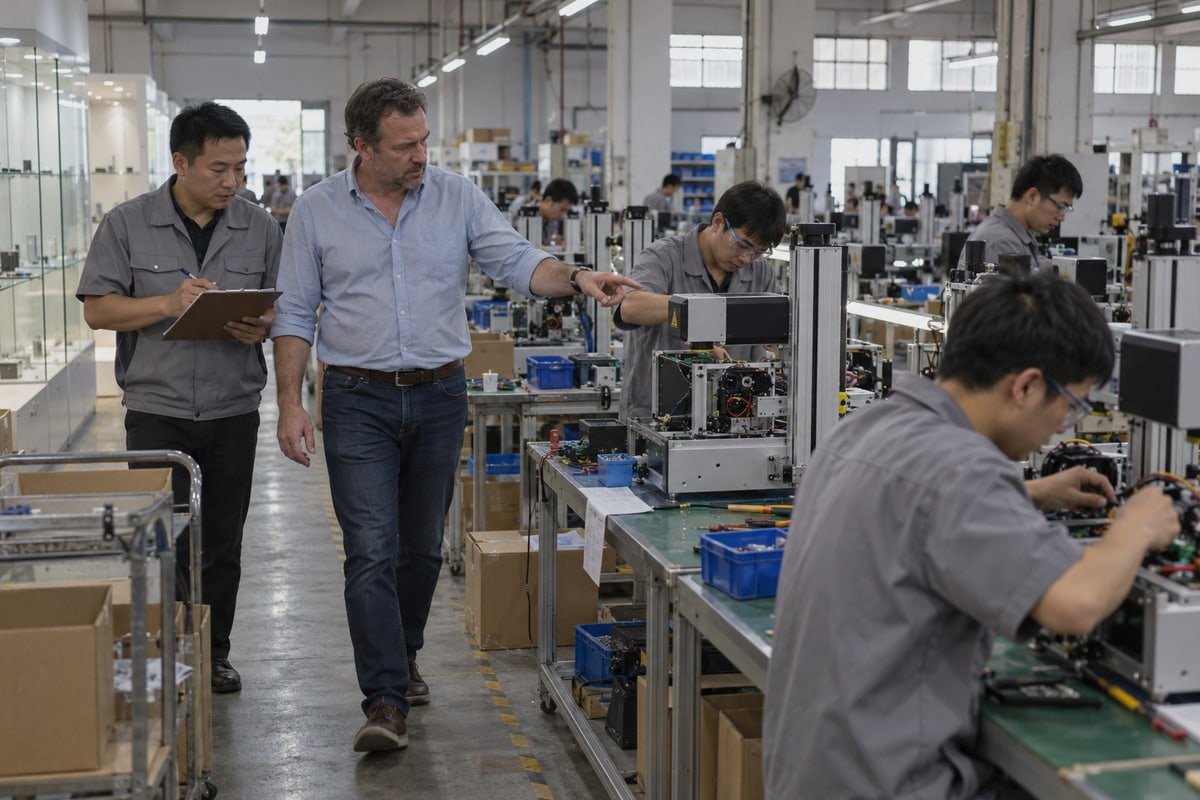
During a recent factory audit, the visitor ignored our showroom and walked straight to the assembly floor to count machines in progress. That was the right move.
Verify actual production capacity by requesting 12–24 months of production records for the CCD laser marking machine model you need, checking the largest order completed, on-time delivery rates, active lines and shifts, and confirming these figures through a factory audit or live video inspection.
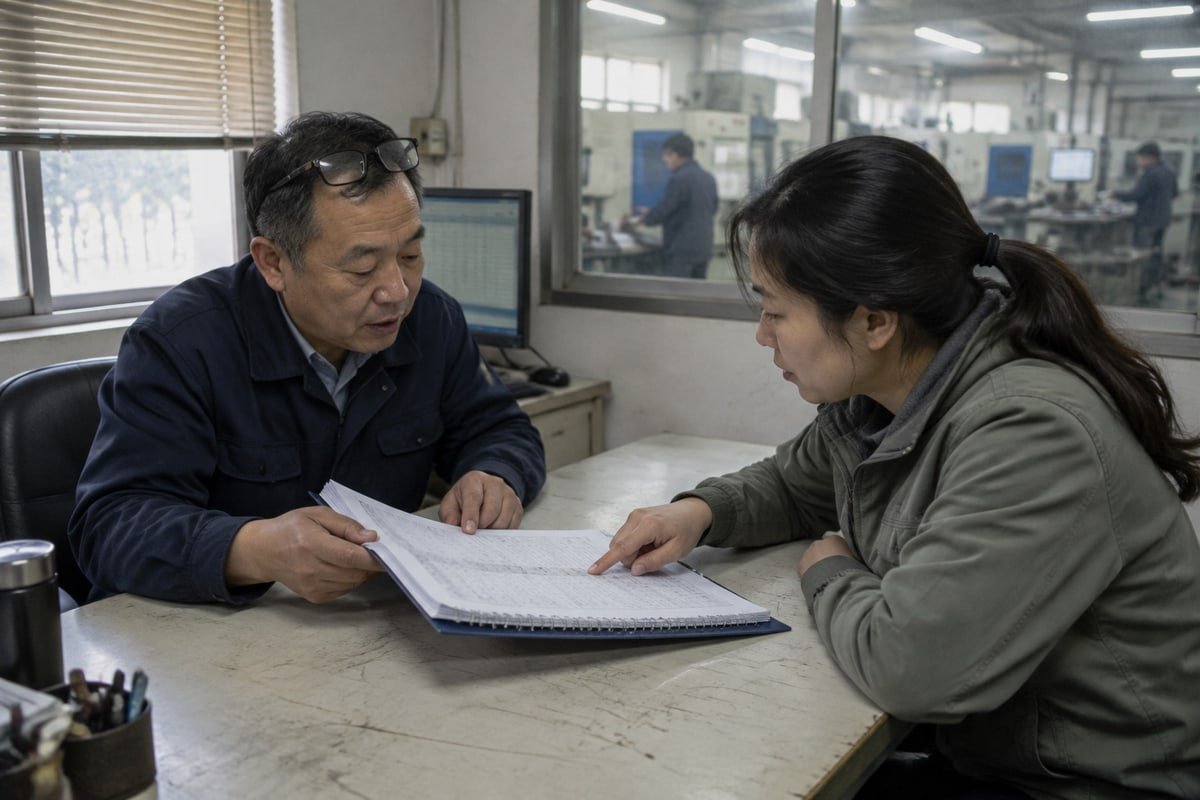
The first thing I tell buyers is simple. Do not ask whether a supplier can fulfill your order. Ask what comparable order it has fulfilled recently, under what conditions, and with what quality results. A sales estimate is not evidence. A production log is.
Four kinds of capacity that get confused
Most capacity disputes start because two people use the same word for different things. Here is how I separate them.
| Capacity type | What it means | How to verify it |
|---|---|---|
| Nominal | The maximum number the supplier claims it can build | Treat as a starting point only |
| Demonstrated | Units actually delivered recently, with documented quality and on-time performance | Monthly production records, delivery logs |
| Scalable | Volume reachable after adding shifts, equipment, workers, or space | Written expansion plan with timelines and costs |
| Sustainable | Volume held for multiple quarters without rising defects or delays | Warranty rates and delivery data over time |
Demonstrated capacity is the number I care about most. So the first personal check I apply is this: look at recent production records and confirm the real monthly output of the CCD automated laser marking machine, not the brochure figure.
Define your order profile first
Capacity cannot be judged without a demand model. Before any supplier conversation, write down your initial quantity, your monthly or quarterly release schedule, your laser type and power, your CCD camera and vision requirements 2, your integration needs, and your acceptance-test expectations. A supplier that can build 100 standardized desktop units may fail at 30 customized inline vision-guided laser systems. Complexity-adjusted capacity is more meaningful than unit counts.
Ask how the number was calculated
I like a simple model. Effective capacity equals theoretical capacity multiplied by labor availability, equipment availability, material availability, and quality yield. If a supplier cannot explain each factor, the headline number is a guess. The market is growing, with several forecasts placing laser marking equipment 3 on a 7–10% annual growth path. Growth means every credible supplier is busy. Your order competes for the same floor space as everyone else's, so demand to see utilization, not just capability.
Finally, confirm you are dealing with a genuine manufacturer. A trading company cannot control scaling. Ask to see in-house R&D staff, machining, and optical assembly during the factory audit.
What questions should I ask to check if a supplier can handle increased order volumes without delays?
A buyer in Italy once sent me a single question over WhatsApp: "What happens if I double the order?" That question deserves a plan, not a promise.
Ask about current monthly output, the largest comparable order, on-time delivery percentage, single-sourced components, stock of fiber laser sources and CCD cameras, test-station count, application engineer headcount, outsourced processes, and the specific steps, costs, and timelines needed if your demand rises by 50%.
Good questions force specific answers. I have grouped the ones I find most useful by the problem they expose. The right column shows what a credible answer sounds like.
| Theme | Question to ask | What a strong answer looks like |
|---|---|---|
| Throughput | What is your current monthly output for this machine family? | A number with records, split by model |
| History | What was your largest comparable order, and when? | Anonymized order data or a reference |
| Lead time reliability | What percentage shipped on time in the last 12 months? | A percentage plus the main causes of delay |
| Component sourcing | Which parts are single-sourced, and which have lead times longer than your quoted delivery? | A bill of materials with vendor lead times and qualified substitutes |
| Inventory | What laser sources, CCD cameras, and control systems are in stock today? | Current stock list, not a warehouse tour |
| Testing | How many machines can be on final test at once? | A bench count and the hours per acceptance test |
| People | How many application engineers support this product? | Headcount by role, not a total employee figure |
| Scaling | What exactly changes if I increase volume by 50%? | Actions, costs, hiring timelines, interim controls |
Check the core component shelf
My second and third personal checks sit here. Ask whether the supplier can add production lines, equipment, or staff fast enough to lift output. Then confirm that the critical parts, meaning the fiber laser source 4, the CCD camera, and the control system, can be supplied on time. A laser marking machine is only as fast to build as its slowest part. If the supplier orders lasers only after your deposit clears, your lead time includes the laser maker's lead time, whether anyone says so or not.
Ask about emergency orders
My fourth check is about pressure. Ask whether the supplier has handled large or urgent orders before, and then verify the delivery record for those orders. Anyone can perform well on a calm schedule. Rush orders reveal whether a factory has slack, backup vendors, and disciplined planning.
Break the lead time into stages
A promise like "30 days after deposit" is weak. Ask for a milestone plan covering engineering review 5, procurement, fabrication, assembly, software configuration, calibration, application testing, factory acceptance, packing, shipping, and commissioning. Ask which step is the critical path. When we quote in our factory, long-lead parts and test time are shown separately, because that is where delays usually hide.
My fifth check closes the loop. Request a written contingency production plan, and put delivery dates and quality standards into the contract. Include delay notification rules and a clear split between customer-caused and supplier-caused delays.
How do I evaluate a supplier's factory, equipment, and workforce to ensure they can scale with my business?
When we plan a surge order, I weigh adding a second shift against hiring new assemblers. The shift is faster, but trained optics technicians cannot be rushed.
Evaluate the factory by walking the full build workflow from incoming inspection to final test, counting assembly bays and test benches, confirming in-house versus outsourced processes, reviewing quality management system records, and checking headcount by skill, especially application, controls, and service engineers.
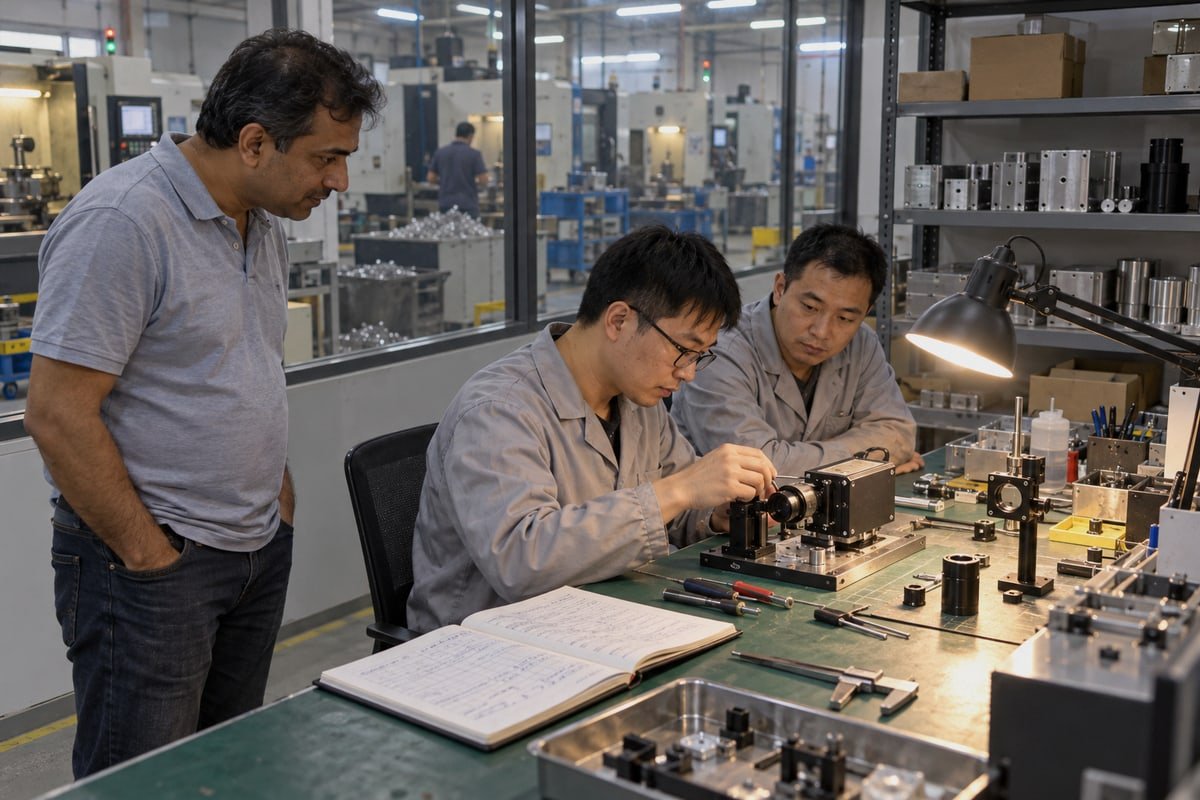
A factory audit is not a tour. It is a sequence of checks. Here is the order I would follow, whether on site or over a live video call.
A five-step factory walk
- Follow the workflow. Trace incoming inspection, machining, optical assembly, electrical panel build, CCD camera integration, software loading, calibration, safety validation, marking trials, final inspection, and packing. Ask which step is the bottleneck and what the normal takt time per machine is.
- Count the physical constraints. Count assembly bays and test benches. Ask if test stations are shared with other product lines. Ask whether floor space exists for a surge batch.
- Separate in-house from outsourced. Outsourcing is not a weakness by itself. But the supplier should name each outsourced process, explain how subcontractors are qualified, and show backup arrangements.
- Inspect the quality management system in action. Certificates are a start. Records are proof. Ask for inspection plans, calibration certificates, final-test forms, nonconformance reports, and corrective actions. Look for Statistical Process Control data on marking consistency across batches.
- Test the vision system on your parts. For vision-guided laser systems, repeatability and accuracy must be proven on production-representative samples. Run a throughput stress test and watch whether the read rate holds during continuous operation.
Workforce by skill, not by headcount
A total employee count hides the real constraint. In our Dongguan plant we have 100 people, including 20 solution design engineers, and I can tell you the engineers are the first resource to run short when custom orders arrive together.
| Role | Why it limits scaling | What to ask |
|---|---|---|
| Assembly workers | Easiest to add, but need training on optics handling | Training time for a new hire |
| Optics and calibration technicians | Scarce; every CCD machine needs camera-to-laser alignment | How many machines each can calibrate per week |
| Application engineers | Required for customer-specific vision algorithms and marking trials | Engineer-to-order ratio |
| Controls and software staff | Needed for PLC, MES, and database integration | Whether a validated platform is reused or redesigned |
| Field-service technicians | Define the technical support infrastructure after delivery | Ratio of engineers to installed machines, regional spare parts |
The large-versus-small objection
Buyers often ask me whether a bigger factory is simply safer. Large suppliers do bring purchasing leverage and formal systems. But they can also be rigid on customization, slow to decide, and inattentive to mid-size orders. Smaller specialists give direct access to senior engineers and faster customization, but they can depend on a few key people and thin spare-parts stock. The answer is not size. It is whether the specific resources your order needs, from fiber laser source stock to automated visual inspection at final test, exist in depth with backup. Ask about telemetry for fleet health monitoring and whether image processing runs locally at the edge, since both affect how a large installed base behaves later.
What red flags should I watch for that indicate a supplier can't reliably scale up CCD laser marking machine production?
Early on, I learned that a huge warehouse impresses visitors but proves nothing. What matters is whether the right laser source is on the shelf today.
Red flags include identical lead times for standard and custom machines, no engineering review allowance, overtime as the only scaling plan, vague factory testing, single-sourced lasers or cameras with no stocked alternatives, inability to state machines currently in production, and refusal to put delivery dates in the contract.
Red flags rarely appear as outright lies. They appear as vagueness. The table below lists the ones I would act on, and what to ask instead.
| Red flag | Why it matters | What to ask instead |
|---|---|---|
| Same lead time for standard and custom machines | Custom CCD work needs engineering approval and extra trials | Show me the milestone schedule for my configuration |
| Shipping time excluded from the quote | Lead time reliability collapses at the port | What is the door-to-door date? |
| Delivery depends on parts not yet ordered | Your schedule is the laser vendor's schedule | Which long-lead parts are in stock today? |
| Overtime is the main scaling strategy | Fatigue raises defects and burns out calibration staff | What is the second-shift or hiring plan? |
| Cannot state how many machines are in production now | Planning data does not exist | Show me the current work-in-progress list |
| Excess inventory offered as proof of capacity | May signal obsolete parts or poor planning | Which exact components for my machine are stocked? |
| Contract silent on delivery and quality | No recourse when delays happen | Write milestones, delay notification, and acceptance criteria into the contract |
The lowest-price objection
A common pushback I hear is that the lowest unit price wins. I disagree, and the reason is total cost. A low price can be eaten by commissioning delays, inconsistent marking quality, software instability, long spare-parts lead times, and production downtime. Our pricing sits in the mid-to-high range, and I say that openly because the difference pays for engineering depth and test time that cheap builds skip.
A scorecard that resists charm
To keep judgment honest, score suppliers with evidence. A practical weighting is: demonstrated production capacity 20%, component sourcing resilience 15%, quality and process control 15%, CCD application performance 15%, lead time credibility 10%, engineering and customization 10%, installation and after-sales service 10%, and financial continuity risk 5%. Score each item from 0 (no evidence) to 5 (independently verified, repeatable performance). Add gates for non-negotiables such as safety, traceability, and application-test results.
Release volume in stages
Finally, do not buy the full volume at once. Run a pilot of one or a few machines for application validation. Place a qualification batch to test repeatability, documentation, and service response. Then tie volume release to demonstrated performance, and keep reviewing delivery, defects, commissioning time, and warranty claims. Ask about software API maturity for emerging Digital Product Passport traceability, because scaled marking is increasingly about data as well as production throughput.
Conclusion
Scaling risk is real, and delays hurt. Check records, components, people, and contracts before you commit. Then release volume in stages, as we do with our own customers.
Footnotes
1. ISO 9001 is the international standard for quality management systems in manufacturing. ↩︎
2. Wikipedia provides a technical overview of machine vision systems and CCD camera requirements. ↩︎
3. Statista provides authoritative market data and growth forecasts for the laser marking industry. ↩︎
4. IEEE is a leading professional association for electronic technology and laser source standards. ↩︎
5. PMI is the global authority on project management, including milestone planning and engineering reviews. ↩︎