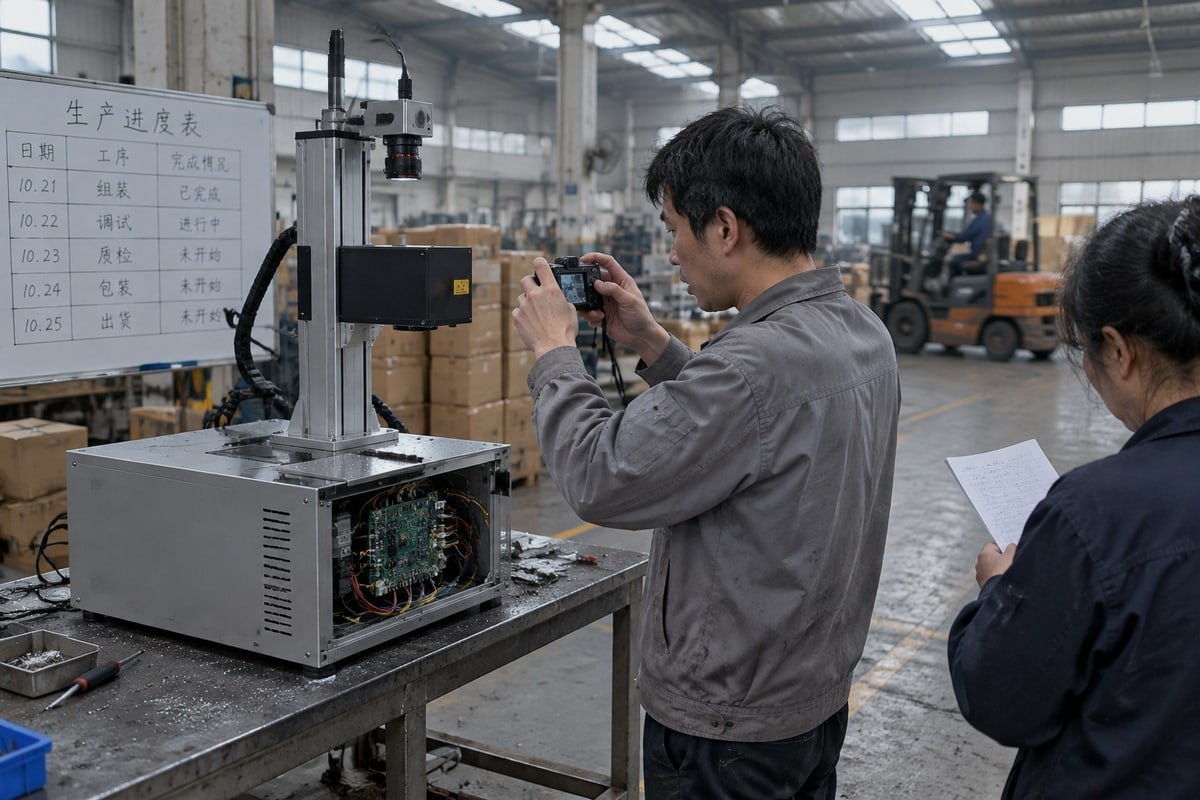
Deposit paid, line waiting, and the only update is “in production.” Our Dongguan factory hears this often, so we now track CCD laser marking machine order status differently.
Track the production status of CCD laser marking machine orders by requesting weekly reports tied to milestones: material preparation, assembly, debugging, and quality inspection. Ask for dated photos or videos at each stage, compare planned and actual dates, and demand an immediate report plus a fix whenever a problem appears.
That is the short version. Below I break it into four questions. What should a real update contain? How do you reach the right person? Which stages matter? And how do you know if the date is slipping before it is too late?
What Information Should I Expect in a CCD Laser Marking Machine Production Update?
Last spring a Swedish buyer forwarded me a competitor’s update. It said “80% done.” Our engineers could not tell what that meant, and neither could he.
A good CCD laser marking machine production update names the current stage, lists what is complete and what remains, shows dated photos or video, flags any blocker, states the next milestone date, and names the responsible person. Percentages alone are not enough; every claim needs evidence.
A percentage is a feeling. A milestone is a fact. That is the whole difference. When I write a weekly report for a customer, I force it to answer five questions. Where is the order now? What is done? What remains? Is anything blocking us? Has the finished work passed its checks? If a report cannot answer all five, it is not a report. It is a reassurance.
The fields every update should contain
| Field | What it means for your order | Evidence you should ask for |
|---|---|---|
| Order number and machine model | Confirms the update belongs to your machine, not a generic one | Serial plate photo once assigned |
| Current stage | Material preparation, assembly, debugging, or quality inspection | Dated photo of that stage |
| Completed items | Specific tasks closed since last week | Short video or photo per item |
| Remaining items | Tasks still open before the next gate | Written list with owner |
| Blockers | Late parts, missing customer files, failed tests | Written description and planned fix |
| Next milestone date | Planned date for the next gate | Same date as the master schedule |
| Required customer action | Samples, drawings, approvals, payment | Deadline for your reply |
Photos that prove the machine is yours
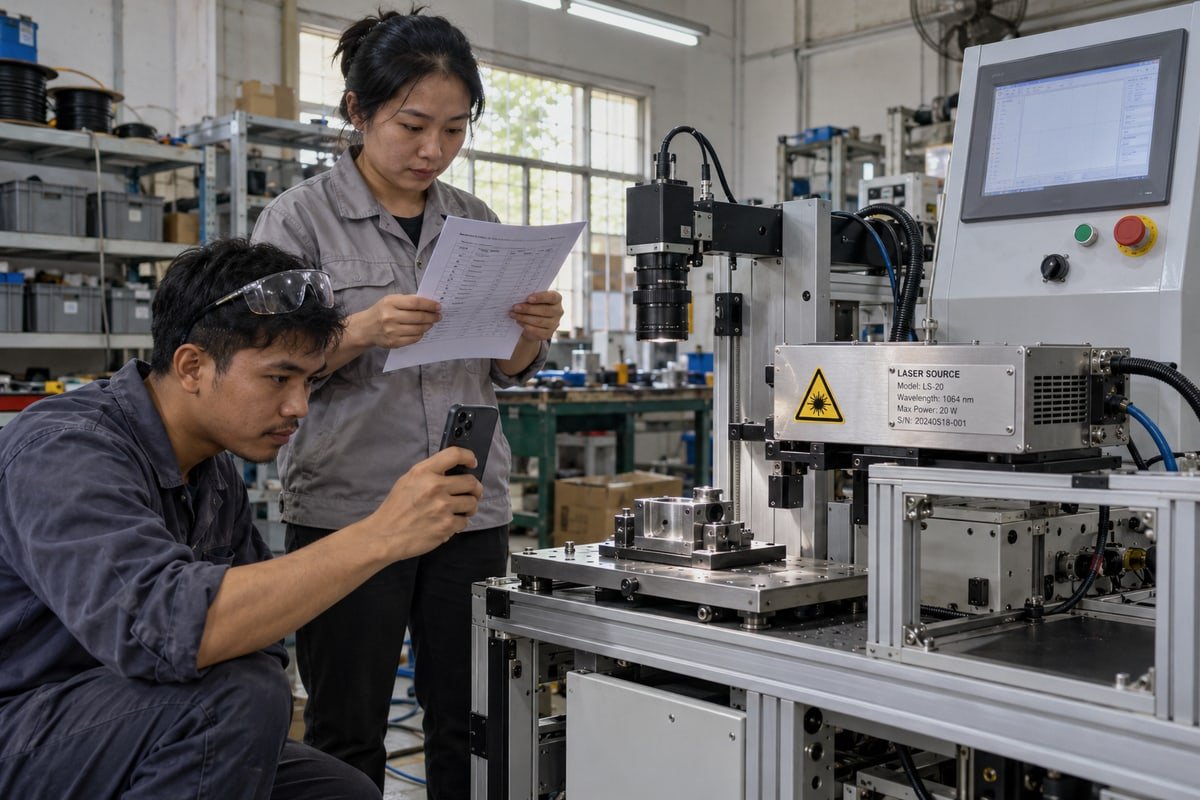
A photo of a machine frame tells you little. A photo of your machine tells you a lot. I ask our workshop to shoot pictures that show identifying details. The laser-source label with its model. The CCD camera and lens assembly. The control cabinet. The fixture or rotary axis built for your part. The HMI screen with your software functions visible. A generic marketing photo should never pass as a progress photo.
The “proprietary drawings” objection
Buyers often ask us for full CAD files 1, and some suppliers refuse on the grounds that the design is proprietary. I understand both sides. Our 20 solution design engineers do not hand out every internal drawing. But that is not an excuse to withhold what you need for approval. You should always receive the machine layout, interface dimensions, utility requirements, the critical-component list, and a vision-interface screenshot. Protecting intellectual property and confirming function are two different things. A good supplier gives you enough to approve, not enough to copy.
How Can I Contact My Supplier to Check My Laser Marking Machine Order Status?
Speed versus record-keeping is a trade-off we weigh daily. WhatsApp answers in minutes; email keeps the decision. Our project team uses both, for different reasons.
Contact your supplier through one named project contact, agree on a weekly reporting day, and use WhatsApp or WeChat for quick questions while confirming every decision by email. Ask whether a customer portal, shared spreadsheet, or order management system is available for milestone tracking.
The worst situation I see is a buyer talking to three different people. Sales says one date. The engineer says another. The shipping clerk says a third. Nobody is lying. They just see different parts of the order. So the first thing I set up with a new customer, whether in Italy, the USA, or Vietnam, is one project contact. That person owns the schedule and the answers.
Communication channels compared
| Channel | Best use | Weakness | How common today |
|---|---|---|---|
| WhatsApp or WeChat with account manager | Quick questions, photos, short videos | Easy to lose decisions in chat history | Standard for export orders |
| Approvals, change orders, dates, acceptance criteria | Slower replies | Standard | |
| Shared spreadsheet | Milestone, planned date, actual date, owner, evidence | Needs discipline to update | Common for single machines |
| Customer portal with automated notifications | Alerts at sourcing, assembly start, final calibration | Depends on supplier IT investment | Growing, not universal |
| ERP or MES push to dashboard | Real-time production monitoring of work in progress | More useful for repeat orders than one-off machines | Varies widely by supplier |
| Live-stream webcam, digital twin, blockchain provenance, AI-predicted ETA | High-transparency “virtual floor walks” and dynamic delivery dates | Rare, expensive, and sometimes marketing talk | Emerging only |
My honest view: do not choose a supplier because of a digital twin demo. Choose one who answers on the agreed day with evidence. The simple tools, used consistently, beat the fancy tools used once.
Set the weekly reporting rhythm
Our rule is one report every week, same weekday, same format. The buyer never has to chase. If a report is late, that itself is a signal. Between reports, chat is for questions. Any answer that changes the specification, a component, a date, or an acceptance criterion gets repeated in email the same day. That email becomes the record.
Build an exception path before you need it
Agree in advance how problems are reported. At our factory the rule is simple. Any abnormal event is reported immediately, not at the next weekly report. The message must include three things: what went wrong, the proposed solution, and the completion time for that solution. A problem without a fix date is only half a report. This mechanism protects both sides. The buyer hears bad news early, and we are forced to think about recovery before we type the message.
What Are the Typical Production Stages I Should Track Before Shipment?
One lesson cost us a late shipment to Turkey: the frame was done, but an imported fiber laser source 2 was still at customs. Visible progress hid the real risk.
Track four core stages: material preparation, mechanical and electrical assembly, debugging with CCD vision calibration, and quality control inspection ending in a factory acceptance test. Add order confirmation at the front and packing at the end, and request dated evidence when each stage closes.
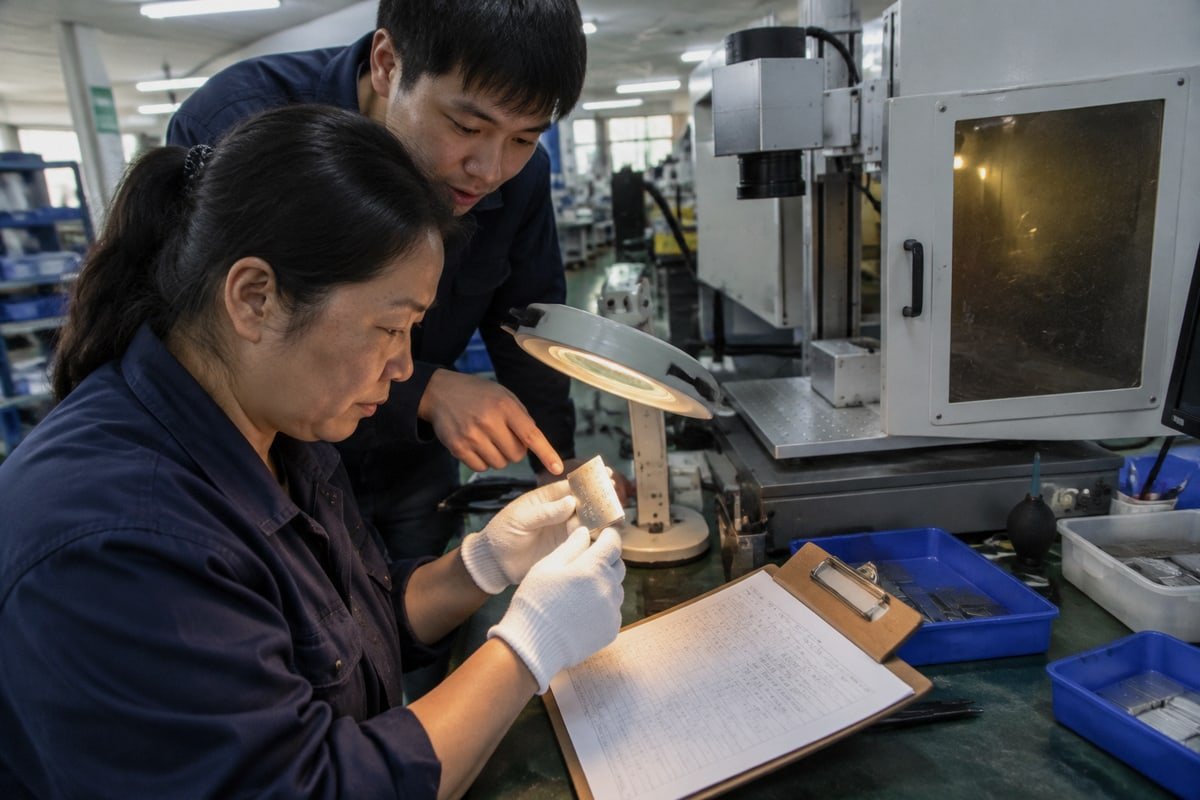
A CCD machine is not a catalog product. Your order may specify the laser wavelength, the marking field, the camera resolution, the lighting, the fixture for an irregular part, barcode reading, auto-focus, and PLC or MES communication. Each of those adds a place where a delay can hide. So I track the stages below separately, and I never let “materials prepared” stand in for “every long-lead part is on the shelf and tested.”
The stages and the proof for each
- Order confirmation and technical review. The specification sheet, layout drawing, laser and camera configuration, sample criteria, and schedule are signed off. The delivery clock start is written down here.
- Material preparation. Long-lead parts are tracked by name: laser source, galvanometer scanner 3, F-theta lens, CCD camera, industrial PC, motion controller, servo motors, lighting, safety parts. Each one is marked ordered, received, inspected, backordered, substituted, or awaiting your approval. This is where supply chain transparency matters most.
- Assembly. Frame, enclosure, optics mounting, camera installation, fixture, wiring, control cabinet, safety interlocks, serial-number plate.
- Debugging and vision integration. Camera and lens calibration, lighting adjustment, pattern recognition, position correction, marking-file import, code reading, recipe management, external communication.
- Quality control inspection and factory acceptance test. Sample marking on your real parts, then the formal FAT gate.
- Packing and dispatch. Final inspection, preservation, crate, packing list, manuals, spare parts, certificates, freight booking.
| Stage | Dated evidence to request | Common hidden delay |
|---|---|---|
| Material preparation | Photo of laser-source label and camera box with model | Imported part still in transit |
| Assembly | Overall frame, cabinet, fixture, serial plate photos | Fixture redesign for part tolerance |
| Debugging | Video of vision-guided laser marking on your workpiece | Recognition fails on reflective or dark parts |
| Quality inspection and FAT | Position accuracy, cycle time, recognition rate, software version | Acceptance criteria never agreed |
| Packing | Photos of packed machine and crate labels | Manuals or certificates not ready |
Why “camera installed” is not “vision validated”
A camera bolted to a machine is hardware. A working automated visual inspection and positioning system is proof. The question that matters is simple. Does the CCD system find the required feature on your part every time, and does it place the mark inside the agreed tolerance? I ask our engineers to record a video with the buyer’s real samples, including deliberately misaligned parts, so the customer sees the correction happen. A clean, flat demo part proves almost nothing about your production component.
The FAT objection, and the fair answer
Suppliers sometimes argue that a factory test cannot copy every condition in your plant. That is partly true. The fair answer is a written test protocol agreed before testing. You send representative samples: normal parts, minimum and maximum dimensions, difficult finishes, worst-case positions. The protocol lists what will be measured. Conditions outside the agreed specification 4 are excluded in writing. Then “working” means the same thing to both of us.
How Do I Know If My CCD Laser Marking Machine Order Is on Schedule?
An Italian customer once asked me a blunt question on WhatsApp: “Stella, is it late or not?” He did not want reassurance. He wanted two dates side by side.
Your order is on schedule when each milestone’s actual completion date matches its planned date on the agreed schedule. Calculate schedule variance as actual date minus planned date for every stage. A positive variance on material preparation or debugging is the earliest warning of a late shipment.
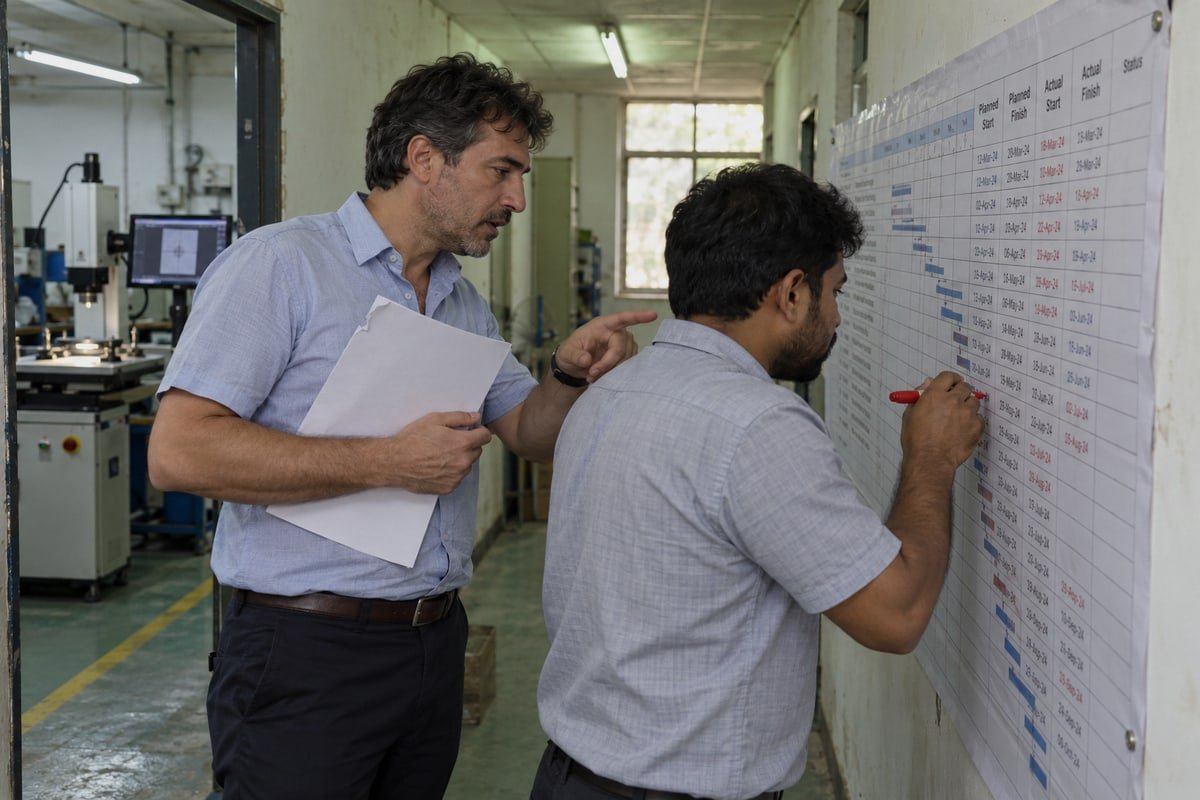
You cannot judge a delay without a baseline. That is why I refuse to quote a manufacturing lead time without also stating when the clock starts. Does it start at deposit receipt, at drawing approval, or at sample receipt? Each answer gives a different ship date. Write it into the order. Then every weekly report shows the plan and the actual side by side.
A worked example, clearly illustrative
The table below is a fictional order, not industry data. It shows how I present the comparison to a customer.
| Milestone | Planned date | Actual date | Schedule variance | Status |
|---|---|---|---|---|
| Technical approval | Day 5 | Day 7 | +2 days | Customer sent revised logo file late |
| Material preparation complete | Day 20 | Day 20 | 0 | On plan |
| Assembly complete | Day 32 | Day 32 | 0 | On plan |
| Debugging and vision calibration | Day 40 | Day 44 | +4 days | Reflective part needed new lighting |
| FAT passed | Day 45 | Day 48 | +3 days | Recovered one day by parallel packing prep |
| Dispatch | Day 50 | Day 52 | +2 days | Partial recovery, customer informed on Day 41 |
Notice two things. First, the delay showed up on Day 41, not on Day 50. Second, the customer heard about it the same day, with a cause, a fix, and a new date. That is the difference between a managed delay and a surprise.
Classify the cause before you argue about the fix
Every delay I report falls into one of four buckets. Customer-caused: late samples, drawings, approvals, or payment. Supplier-caused: staffing, assembly, procurement, or quality failures. External: customs, transport, component shortages. Scope-related: new features requested after the order. Naming the bucket cools the conversation and points to the right remedy. For a scope change, the answer is a written change order with a revised date, not an apology.
Warning signs that the date is drifting
Watch for repeated “almost finished” messages with no milestone evidence. A delivery date that moves without a revised full schedule. Vague phrases like “testing soon.” Refusal to name the laser source or camera brand. Substitutions you never approved in writing. A FAT run only on generic samples. Pressure to pay the balance before the agreed test. Shipment announced while manuals and spare parts are still missing.
After dispatch, keep tracking
“Ready to ship” means we have passed our internal gates. It does not mean you have the machine. Record the carrier, booking number, bill of lading 5 or air waybill, departure date, and estimated arrival. Then plan installation, training, and the handover to post-sales technical support, including remote diagnostics access. For repeat buyers, I also suggest a simple metric: on-time delivery rate equals orders shipped by the agreed date divided by total orders, times 100. Keep it per supplier. It tells you more than any brochure.
Conclusion
Vague updates waste your deposit and your line time. Ask us for a milestone schedule with weekly evidence before you order, and “in production” will finally mean something.
Footnotes
1. This ISO standard specifies the general principles for technical drawings and digital CAD documentation. ↩︎
2. ScienceDirect offers comprehensive technical overviews of fiber laser technology and its industrial applications. ↩︎
3. ScienceDirect provides technical definitions and engineering principles for galvanometer scanners used in laser systems. ↩︎
4. ISO 9001 is the global standard for quality management systems and technical specifications in manufacturing. ↩︎
5. Official U.S. Customs and Border Protection guidance on essential documentation for international trade and shipping. ↩︎