
Picking a CCD laser marking machine for your product lineup feels like a gamble. Misjudge it and you pay for a camera nobody uses. Our Dongguan team tests fit first.
A CCD laser marking machine fits your product lineup when parts arrive with positional or angular variation, SKUs change often, marks must align with existing features, and misplaced marks are costly. If every part is rigidly fixtured and identical, a conventional laser marker is usually the better buy.
The decision has two halves. One half is technical: shapes, materials, volume, and integration. The other half is commercial: whether your customers, your margins, and your existing equipment line actually call for vision positioning. I will walk through both. Let’s start with the physical products.
What Product Shapes and Sizes Can a CCD Laser Marking Machine Handle?
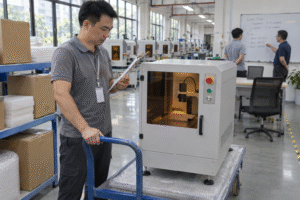
Last spring a tray of stamped brackets landed on our trial bench, every piece rotated differently. The camera found them all. That trial changed how I explain shape fit.
A CCD laser marking machine handles flat, small, irregular, and multi-SKU parts placed loosely within the camera's field of view, compensating for rotation and offset. Curved, tall, or multi-sided products need extra hardware such as a rotary axis, height sensor, or 3D vision for reliable results.

Shape decides hardware. Size decides optics. I keep the two apart because buyers often blur them. A tiny flat connector and a large flat panel both suit a visual positioning system, but they need different lenses. A cylindrical tool shank may be small, yet it still needs a rotary axis. The table below is the quick sort we use when a new inquiry arrives.
Shape categories and what each one needs
| Product geometry | CCD fit | What usually has to be added |
|---|---|---|
| Flat parts with little height variation (PCBs, nameplates, hardware tools) | Strong | Standard camera and lens |
| Small parts in trays or loose bulk (electronic components, connectors) | Strong | Higher-resolution camera, narrower field of view |
| Irregular stamped or molded parts (auto parts, brackets) | Strong | A trained recognition recipe per SKU |
| Cylindrical parts (tubes, shanks, battery cells) | Conditional | Rotary axis synchronized with the scanner |
| Curved or warped surfaces | Conditional | Height sensor or 3D vision for focal compensation |
| Recessed or multi-sided products | Weak on its own | Multiple cameras or a repositioning station |
Field of view versus the smallest feature
The camera must see the whole recognition area in one frame. It must also resolve the smallest fiducial or edge 1 you want it to find. Those two goals pull against each other. A wide field of view covers a full tray. A narrow field of view gives finer pixel detail for product orientation detection on small electronic components. On our trial bench we check both before we suggest a lens. If one frame cannot do both jobs, we look at a second camera or at indexing the tray under a fixed camera.
Working distance matters too. The galvanometer scanner has a fixed focal plane 2 for a given lens. Vision tells the scanner where to aim in X, Y, and rotation. It cannot stretch depth of focus. Ranking pages now describe 3D vision sensors that feed depth data for dynamic Z-axis compensation on warped surfaces. That is real technology, but it is extra hardware and extra cost. Ask for it only when your parts are truly uneven or stacked at different heights.
What vision cannot fix
Here is the objection I hear most: "With a camera, I can throw the fixtures away." Not quite. Fiducial mark recognition compensates for moderate rotation and offset inside the frame. It does not fix severe tilt, overlapping parts, or features hidden by the product's own geometry. Glare from polished stainless steel and transparent acrylic can also confuse edge detection. For those cases we still design a simple nest, add diffuse lighting, or fit a polarizing filter. The fixture becomes cheaper and looser. It does not disappear.
Newer AI-driven feature recognition can accept slightly deformed parts that strict pattern matching would reject. We treat that as a bonus for stamped or molded parts with tolerance drift, not as permission to send bad parts to the laser.
Which Materials in My Product Lineup Are Compatible With CCD Laser Marking?
Every week our engineers weigh the same trade-off: a buyer wants one camera-equipped machine for brass, ABS, and PCB boards. The camera says yes. The laser source often says no.
CCD laser marking is compatible with stainless steel, aluminum, copper, brass, titanium, iron, ABS, acrylic, PVC, and electronic components, but compatibility depends on the laser source, not the camera. Pair fiber or MOPA with metals, CO2 with packaging substrates, and UV with heat-sensitive plastics, then test real samples.

The camera does not make an unsuitable laser suitable. That sentence should sit at the top of every material review. A CCD laser marking machine is a laser first and a vision system second. So I always start with the substrate and work backwards to the source.
Laser source first, camera second
| Material group in a typical lineup | Laser source starting point | Common mark result | Vision caution |
|---|---|---|---|
| Stainless steel, titanium alloy, iron products | Fiber | Annealing, deep engraving, serials | Glare on polished finishes; use diffuse lighting |
| Anodized aluminum 3, coated metals | MOPA fiber | Black marking, coating removal, color effects | Dark reference features on dark coatings reduce contrast |
| Copper, brass | Fiber or MOPA at higher power | Logos, lot codes | Highly reflective; polarizing filter helps |
| ABS, PVC, general plastics | Fiber or UV depending on pigment | High-contrast white or dark mark | Dark-on-dark parts need extra illumination |
| Acrylic, packaging, paper-based materials | CO2 | Frosted or surface mark | Transparent edges confuse edge detection |
| PCB boards, electronic components, medical devices | UV | Fine, low-heat text and Data Matrix | Fiducial mark recognition works well on printed pads |
Each row is a starting point, not a promise. Coatings, pigments, additives, and surface finish change results fast. Black marking on anodized aluminum usually calls for the pulse control of a MOPA source. A plain fiber source may frost the same part instead. A dark PVC housing can give poor contrast under one wavelength and a crisp mark under another.
Covering the full lineup, not the category
When we assess a buyer's lineup, we ask for every material, every color, and every coating that actually ships. This is the second check on my own list: confirm the equipment can cover the materials and marking scenarios already present in the product line. A category label like "plastic" tells me almost nothing. Glass-filled ABS behaves differently from unfilled ABS.
The mark type matters as much as the substrate. Serial numbers, lot codes, logos, deep engraving, coating removal, and Data Matrix codes 4 each stress the laser differently. For 2D codes, I ask buyers to agree on a grading method 5 rather than visual approval. ISO/IEC 15415 is the standard most quality teams reference for 2D code quality. A code that looks fine to the eye can still grade poorly under a verifier, and it can fail under the harsh lighting of a customer's scanner.
Where the camera genuinely helps on materials
The camera does not change what the laser does to the surface. It changes how reliably the mark lands on the right part of that surface. On a PCB, fiducial mark recognition lets the code sit beside a component without touching it. On a battery component, the same high-precision alignment keeps the code clear of a weld seam. That is the honest value: placement, not chemistry.
How Do I Match CCD Vision Positioning to My Production Volume and Batch Variety?
A distributor in Italy messaged our team on WhatsApp asking whether his customers truly needed CCD or just liked the word. That honest question is where volume planning should start.
Match CCD vision positioning to your production by counting SKUs, changeover frequency, and positional variation rather than raw volume. High-mix lines with frequent changeovers gain the most; high-volume lines of identical, fixtured parts gain the least, because image capture adds cycle time without removing any real alignment work.

Volume alone is a poor guide. I have seen small shops with constant SKU changes gain more from vision than large plants running one identical part all year. So I compare three configurations, not two. Comparing "laser with camera" against "laser without camera" hides the inspection option that regulated buyers often need.
Three configurations, side by side
| Configuration | Best for | Trade-offs to accept |
|---|---|---|
| Conventional fixed-fixture marker | Identical parts, fixed mark position, rare changeovers, forgiving mark area | A precision fixture per SKU; operator alignment skill; little flexibility for new variants |
| CCD-positioned marker | High mix, loose placement, marks aligned to holes or artwork, multiple SKUs on one station | Higher price, calibration, lighting sensitivity, image capture time, more training |
| CCD positioning plus post-mark inspection | Traceability at part level, medical and automotive compliance, 2D code grading | Highest cost, reject handling, deeper software integration, more maintenance points |
Cycle time is longer than the scan
A galvanometer scanner can finish a small code in a fraction of a second. The full cycle is slower. It includes part arrival, sensor trigger, image capture, image processing, position calculation, marking, verification, and release. For a conveyor, the math is simple. A line running at 60 metres per minute moves about one metre per second. If your full cycle takes half a second, the part has moved half a metre since the trigger. Marking-on-the-fly with an encoder handles this, but only when the image processing software 6 and the scanner are synchronized. Ask the supplier for measured cycle time on your actual part, including camera acquisition, not the catalogue scan speed.
Variety is where the payback lives
For high-mix lines, I treat CCD as a changeover technology first. Ranking pages promise changeovers dropping from hours to seconds. The real gain depends on recipe management. If an operator can select a validated recipe, or the system reads a barcode and loads the right program, batch marking efficiency improves across the whole shift rather than per part. If every SKU still needs manual camera repositioning, you have bought precision but not flexibility.
A simple payback frame keeps everyone honest:
- Annual CCD benefit = avoided scrap + avoided rework + labor savings + changeover savings + quality-related savings
- Annual CCD cost = added purchase price + integration + calibration + maintenance + training + downtime risk
Fill it with real production data. Do not assume the camera saves money because it exists.
The commercial fit check
For distributors and integrators, the questions shift from the line to the market. When we work with partners who already sell MOPA or fiber lines, I ask five things. Do their existing customers have a stated CCD automation need, so the new model does not duplicate their current product positioning? Does the machine cover the materials and scenarios their lineup already serves? Do purchase cost, market selling price, and margin leave reasonable profit? Can it be bundled with existing laser equipment to lift repeat orders? And is the target market growing, with competition they can handle? Those five answers decide fit as much as any specification sheet.
What Customization Options Should I Discuss With My Supplier Before Buying?
The hardest lesson from seventeen export markets: a machine that looks perfect on clean samples can stumble on dusty, oily production parts. Now we ask for worst-case samples before quoting.
Discuss laser source, camera resolution and field of view, lighting and glare control, rotary or Z-axis options, recipe management for multiple SKUs, PLC and MES interfaces, post-mark inspection, Class 1 enclosure safety, spare parts, training, and a written trial protocol with acceptance criteria before signing any purchase order.

Customization is where a CCD laser marking machine either earns its price or becomes shelf furniture. Our twenty solution design engineers spend more time on this stage than on the laser itself. The conversation splits into hardware, software, service, and proof.
Hardware and optical choices
| Customization option | Why it matters | Who should ask for it |
|---|---|---|
| Laser source: fiber, MOPA, CO2, or UV | Sets what the substrate can accept | Everyone; this comes before the camera |
| Camera resolution and lens field of view | Must resolve the smallest fiducial while seeing the whole tray | Small-part and multi-part tray users |
| Lighting: diffuse, coaxial, or polarized | Controls glare on polished metal and transparent plastic | Stainless, brass, acrylic lineups |
| Rotary axis, Z-axis, or 3D vision | Handles cylinders, warped parts, and height variation | Tools, tubes, battery cells, molded housings |
| Enclosure meeting IEC 60825-1 Class 1 conditions | Protects operators during automatic operation | Any line with operator access |
| Fume and particulate extraction | Plastics and coatings release smoke that also fouls the lens | PVC, ABS, coated-metal users |
| Conveyor with encoder synchronization | Enables marking-on-the-fly without stopping the line | Continuous-flow packaging and electronics lines |
Software and industrial automation integration
Ask how recipes are stored, how the system identifies the SKU, and whether it blocks the wrong marking file. Ask for the PLC handshake, the MES or ERP data path, and pass/fail outputs for reject handling. Clarify whether automated optical inspection is included or quoted separately. A machine that can find the mark position may still need a second camera or a verifier to grade the result. Some systems now archive a high-resolution image of every mark as a permanent audit record, and edge-processed analytics can flag feeding problems upstream before they stop the line. Both are useful. Both should be priced clearly.
Service terms that protect you
Delivery timing is a pain point I hear from almost every buyer. Get the ship date, installation responsibility, and calibration responsibility in writing. Confirm spare cameras, lenses, boards, and laser components are stocked. Confirm training scope and warranty exclusions. Confirm who answers when a recognition recipe fails at two in the morning.
A trial protocol you can hold them to
- Supply every material, color, coating, and size in the lineup, plus worst-case dirty samples.
- Write the acceptance criteria before the trial: positional and angular error, smallest text, code grade, cycle time, reject rate.
- Require random placement inside the field of view. No hand-positioned samples.
- Request documented results: recognition success rate, first-pass yield, false-match rate, repeatability across batches, and behavior when no part or the wrong part appears.
- Approve the machine only if it meets the written targets.
Conclusion
Buy a CCD laser marking machine when it solves a measured positioning, changeover, or traceability problem your customers already have. Test real parts, set written targets, then decide with confidence.
Footnotes
1. Reference points or physical boundaries used by vision systems to determine part orientation. ↩︎
2. Optical concept defining the specific distance where a laser beam is perfectly focused for marking. ↩︎
3. Surface treatment for aluminum that creates a durable oxide layer requiring specific laser parameters. ↩︎
4. Wikipedia provides a stable, comprehensive technical overview of Data Matrix symbology and standards. ↩︎
5. Standardized approach for evaluating the quality and readability of 2D barcodes in industrial settings. ↩︎
6. Computational tools used to analyze camera data and calculate coordinate offsets for laser alignment. ↩︎